Project specification

Verified part, tooling and inspection details

Part dimensions180 × 140 × 10 mm
Minimum wall thickness1.4 mm
Critical dimensional tolerance±0.05 mm
MaterialPC
Mould steel / cavities / gating / ejectionS136H · 1+1 cavities · edge gate · direct ejection
Machining equipmentCNC · slow wire EDM · mirror EDM · grinding · milling
Inspection equipmentCMM · 2.5D vision measuring system · profile projector · gauge blocks
Production reference3,000 parts in approximately 3 days after approval
Final quality result96% good part rate
Semiconductor charging equipment case

Thin Wall Charging Station Housing

A production mould for a thin PC housing used in semiconductor charging equipment. Insert moulded nuts and thin sections made filling, local strength and assembly interfaces the key engineering topics.
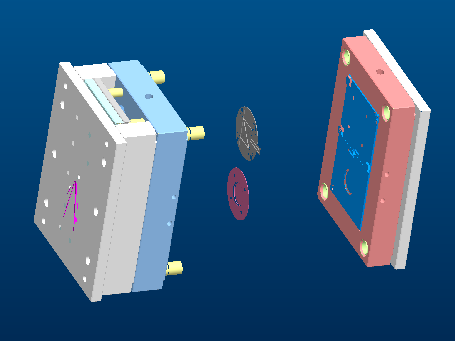
3D mould structure for a semiconductor charging station housing
3D TOOL STRUCTURE1+1 cavity layoutRelease, insert positions and flow were reviewed before steel cutting.
ApplicationSemiconductor charging
MaterialPC
Tool steelS136H
Tooling1+1 cavities
Delivery30 days
01 · Customer need and engineering challenge

A 30 day tooling program for a thin wall housing with insert moulded nuts

The customer required the mould to be delivered within 30 days for a PC charging station housing. The product was thin and included insert moulded nuts, so the project review focused on filling balance, local wall strength, nut position and reliable release.

01
Thin wall fillingThin sections increased the risk of short shots during the first mould trials.
02
Insert moulded nutsNut positions needed sufficient surrounding thickness without visible nut marks.
03
Assembly interfaceThe finished housing had to assemble successfully into the customer's product.
Mould component and insert layout
Moulded PC housing samples
02 · Tooling approach

DFM led tooling with a focused trial correction

TOOL DESIGN

S136H · 1+1 cavities

An edge gate and direct ejection were selected for the approved part and mould layout.

MACHINING ROUTE

Controlled mould construction

CNC, slow wire EDM, mirror EDM, grinding and milling were used for the mould components.

TRIAL FIX

Two trial rounds

Short shots and nut marks were identified during two trials. The nut boss area was thickened to improve filling and local strength.

03 · Result and customer value

Delivered in 30 days and ready for customer assembly

The mould was delivered within the 30 day target. After two trial rounds and the nut boss adjustment, the project reached a final good part rate of 96% and the finished parts were accepted for assembly into the customer's product.

Customer business value
Supported a smooth assembly process and enabled the finished charging equipment product to move into the market.
30 daysMould delivery
2Trial rounds
96%Good part rate
A clear path from drawing to production

Discuss a similar tooling project

Share your 3D data, material and delivery target for a practical DFM and mould review.

DISCUSS YOUR PROJECT →← BACK TO EXPERIENCE