Project specification

Verified part, tooling and inspection details

Part dimensions250 × 150 × 15 mm
Minimum wall thickness1.5 mm
Critical dimensional tolerance±0.05 mm
MaterialPC
Mould steel / cavities / gating / ejectionS136H · 1+1 cavities · edge gate · direct ejection
Machining equipmentCNC · slow wire EDM · mirror EDM · grinding · milling
Inspection equipmentCMM · 2.5D vision measuring system · profile projector · gauge blocks
Production reference3,000 parts in approximately 5 days after approval
Final quality result96% good part rate
Semiconductor charging equipment case

Insert Moulded Charging Station Enclosure

A second PC enclosure program for semiconductor charging equipment. The thin product and multiple insert moulded nuts required careful draft, local reinforcement and repeatable filling through trial correction.
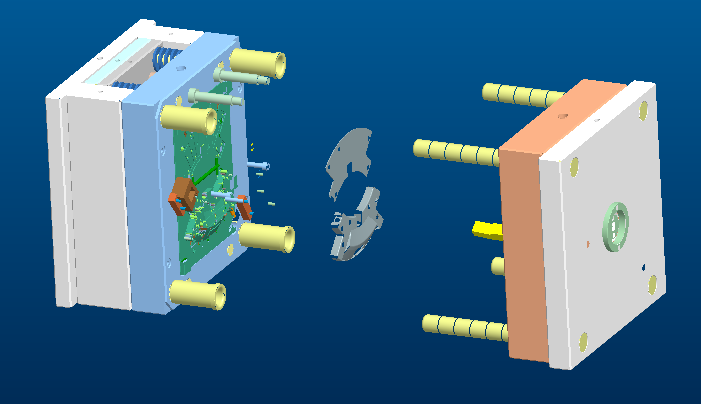
Mould structure for a semiconductor charging station enclosure
MOULD STRUCTURE1+1 cavity toolingInsert positions, release direction and filling were reviewed before machining.
ApplicationSemiconductor charging
MaterialPC
Tool steelS136H
Tooling1+1 cavities
Delivery30 days
01 · Customer need and engineering challenge

Engineering a thin enclosure with multiple insert moulded nuts

The customer required a 30 day mould delivery for a PC semiconductor charging station enclosure. The design combined thin sections with several insert moulded nuts, so the main review topics were filling, draft, local wall thickness and insert stability.

01
Thin product sectionsThin areas required a stable filling route and carefully controlled venting.
02
Multiple insert moulded nutsA larger number of inserts increased the risk of nut marks and incomplete filling around the interfaces.
03
Release and draftDraft was reviewed and increased where necessary to reduce release resistance.
Opened tool view
Mould detail review
02 · Tooling approach

Draft and insert detail refined through three trials

TOOL DESIGN

S136H · 1+1 cavities

An edge gate and direct ejection were matched to the approved PC part and insert arrangement.

MACHINING ROUTE

Five coordinated processes

CNC, slow wire EDM, mirror EDM, grinding and milling supported the mould build and detail finishing.

TRIAL FIX

Three trial rounds

Short shots, nut marks and multiple insert issues were addressed by increasing draft and thickening the nut areas.

Moulded enclosure sample
Assembly side of moulded enclosure
03 · Result and customer value

Stable moulded parts supported a smooth product launch

The mould was delivered within 30 days. Three trial rounds resolved the filling and insert related issues, reaching a final good part rate of 96%. The parts were accepted for assembly and the finished product moved into the market.

Customer business value
Reduced assembly risk around the insert interfaces and supported the customer's planned product launch.
30 daysMould delivery
3Trial rounds
96%Good part rate
A clear path from drawing to production

Discuss a similar tooling project

Share your 3D data, material and delivery target for a practical DFM and mould review.

DISCUSS YOUR PROJECT →← BACK TO EXPERIENCE